
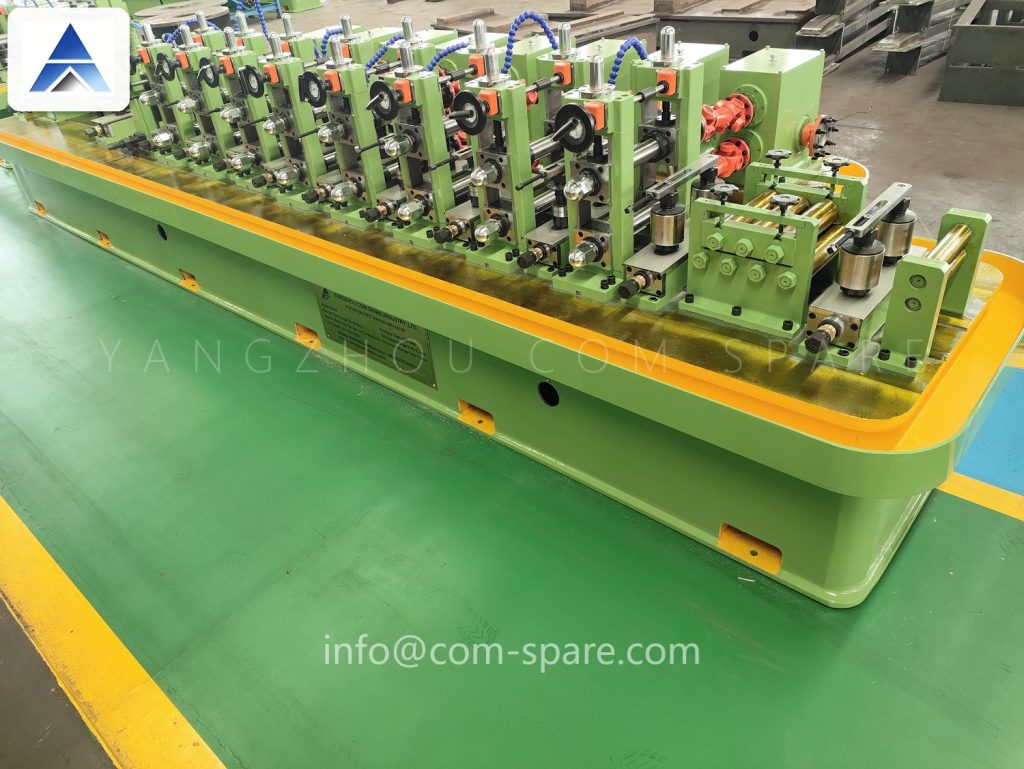
A COMSCO ERW tube mill line is quoted as one system, not a shopping list of stations. The roll tooling, the seam welder and the flying cold saw are built in our own workshops, so the line is configured around the pipe you actually sell — diameter range, wall thickness, line speed and end quality. If you already run a mill and one station is holding your output back, that single station is also a quote.
Configure the line around what you sell, not around the catalogue
A tube mill line is a chain, and a chain is limited by its narrowest link. The useful question at quotation stage is not “what is the biggest model” but “which station will limit me first”. On a line running thin wall at high speed, that is usually the cut-off cycle time. On heavy wall, it is weld power. On a mixed order book, it is the size change.
| If your order book looks like this | The line should be weighted towards |
|---|---|
| One or two sizes, thin wall, high volume | Fast cut-off, big accumulator, high-speed drives |
| Many sizes, short runs | Quick-change stands, pre-set roll sets, fast pass line adjustment |
| Heavy wall structural | Weld power, stand rigidity, heavy saw carriage |
| Thick wall plus tight tolerance | Extra sizing stands, coolant temperature control, in-line gauging |
| Export bundles, few sizes | Automatic stacker and strapping, because labour is the constraint |
We quote the stations separately for exactly this reason. If the budget only covers the mill and the saw this year, the accumulator and the stacker can follow when the volume justifies them — the line is designed so that they bolt on without re-engineering.
Line speed is a range, not a number
Every line has a speed at which it makes saleable tube, and that speed is lower than the maximum the drives allow. A 76 mm mill with a top speed of 90 m/min will usually run 50 to 60 m/min on 2.5 mm wall because the weld and the saw set the pace, not the motor. When comparing quotations, ask for the speed at the smallest and the largest tube in the range, at the wall you actually run. A supplier who quotes one speed is quoting his best day.
The HG series, model by model
Eight models cover ø8 to ø355 mm. The numbers below are the working range we build to; final stand count, motor size and speed are set against your wall and output target, not against the model number alone.
| Model | Tube OD | Wall | Strip width | Line speed | HF power | Roll shaft | Forming stands |
|---|---|---|---|---|---|---|---|
| HG16 | ø8 – 16 mm | 0.3 – 1.0 mm | 25 – 50 mm | 60 – 120 m/min | 60 kW | ø40 mm | 8 – 10 |
| HG32 | ø12 – 32 mm | 0.4 – 1.5 mm | 38 – 100 mm | 50 – 110 m/min | 100 kW | ø50 mm | 9 – 12 |
| HG50 | ø16 – 50 mm | 0.6 – 2.0 mm | 50 – 155 mm | 40 – 100 m/min | 150 kW | ø55 mm | 10 – 14 |
| HG76 | ø32 – 76 mm | 0.8 – 3.0 mm | 100 – 235 mm | 30 – 80 m/min | 200 kW | ø70 mm | 12 – 16 |
| HG114 | ø45 – 114 mm | 1.0 – 4.0 mm | 140 – 355 mm | 25 – 60 m/min | 250 kW | ø85 mm | 14 – 18 |
| HG165 | ø76 – 165 mm | 1.5 – 5.0 mm | 235 – 510 mm | 20 – 50 m/min | 400 kW | ø110 mm | 16 – 20 |
| HG219 | ø114 – 219 mm | 2.0 – 6.0 mm | 355 – 680 mm | 15 – 40 m/min | 600 kW | ø140 mm | 18 – 22 |
| HG355 | ø165 – 355 mm | 3.0 – 10.0 mm | 510 – 1100 mm | 10 – 25 m/min | 900 kW | ø180 mm | 20 – 26 |
Strip width is calculated from the finished tube as W = π (OD − wall) plus a welding allowance, so it is worth checking against your slitting sheet before the roll set is cut. Overlapping ranges are deliberate: an HG114 will run ø45 tube for a customer who also needs ø114, which is usually cheaper than buying two mills.
The jump from HG165 to HG219 is not a scaled-up version of the same machine. Foundation, crane capacity, coil weight and the space needed behind the saw all change the plant design, not just the mill.
Line flow — nine stations
| No. | Station | What it does |
|---|---|---|
| 1 | Uncoiler | Pays off the steel coil and feeds strip into the line at controlled tension. |
| 2 | Shear & Butt Welder | Shears the strip head and tail square, then welds them, so the line keeps running through coil changes. |
| 3 | Strip Accumulator | Stores strip while a new coil is loaded, so the mill never has to stop for a coil change. |
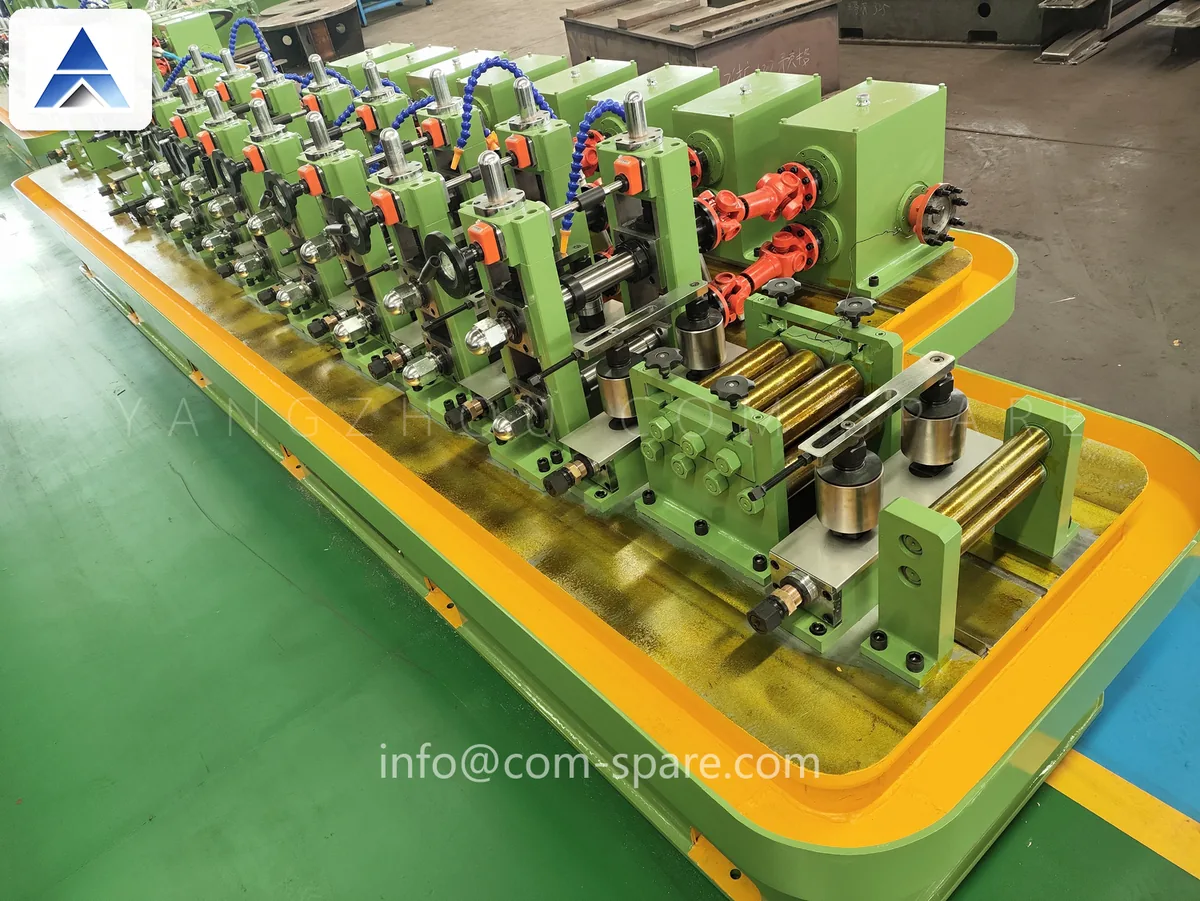
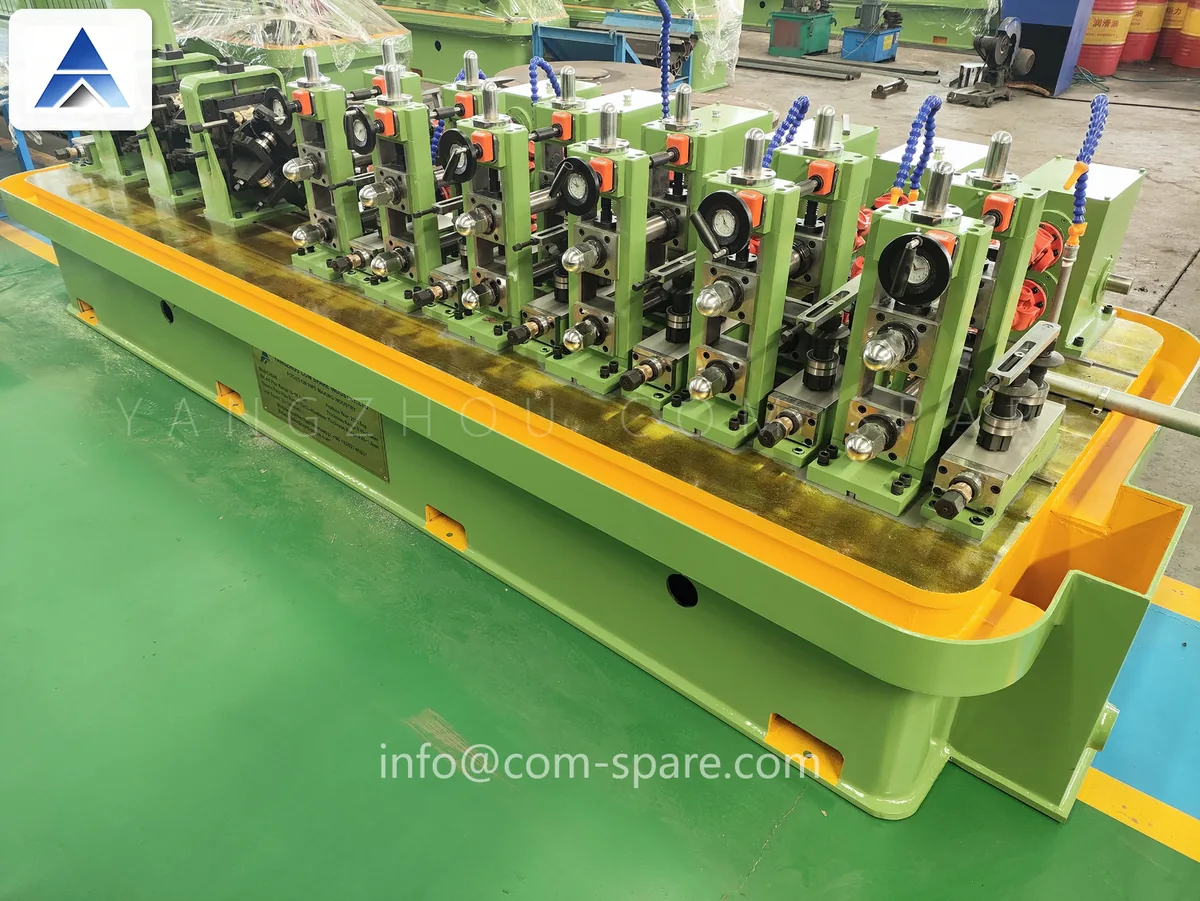
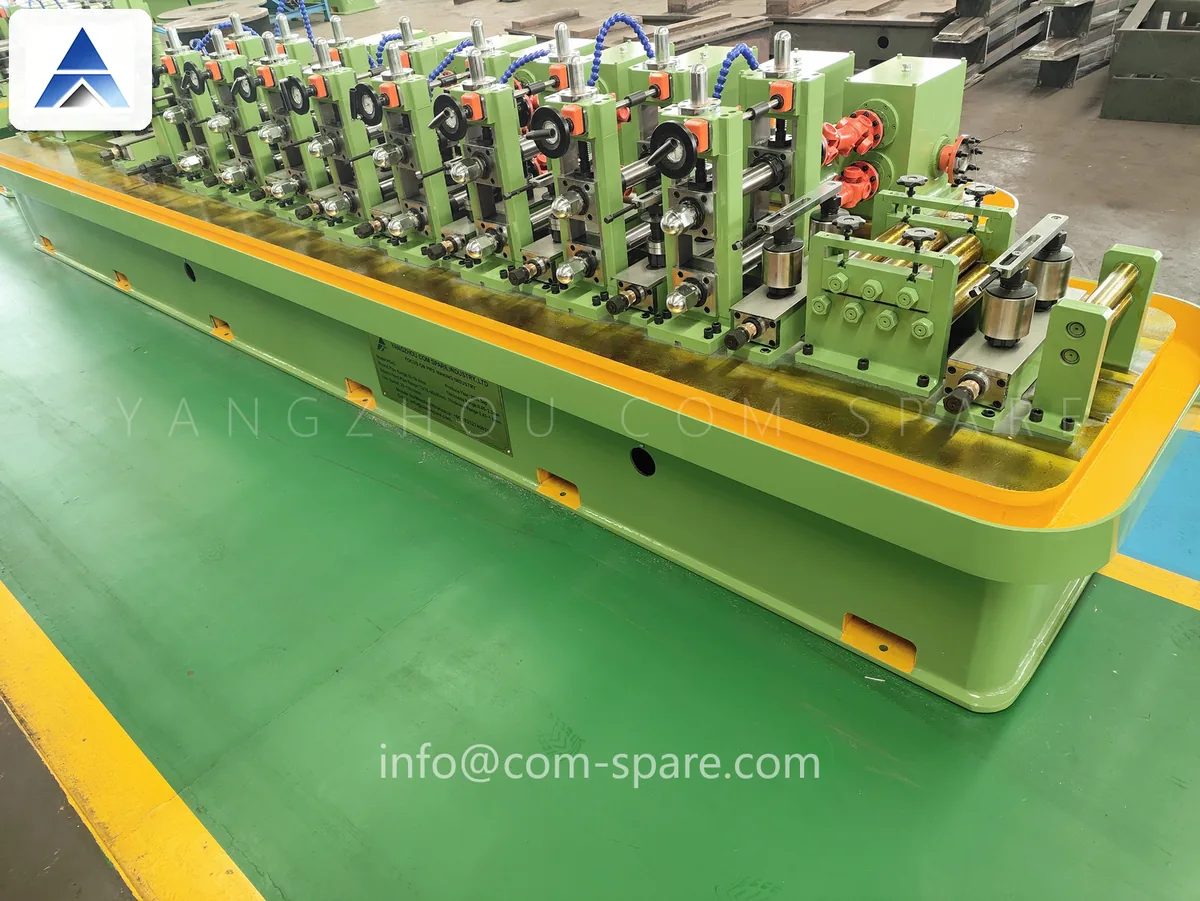
| 4 | Tube Mill — Forming & Sizing | Rolls the strip through breakdown and fin passes, applies the HF weld, then sizes the tube to its final diameter. |
| 5 | Cooling Section | Water-cools the weld and the tube body before sizing and cut-off. |
| 6 | Flying Cold Saw | Travels with the tube and cuts to length with a cold saw blade — square, burr-free ends at full line speed. Built in our own workshop. |
| 7 | Run-out Table | Carries finished tubes away from the saw and gathers them for bundling. |
| 8 | Stacker / Palletizer | Lays cut lengths into neat, stable packs — manual or automatic. |
| 9 | Strapping Machine | Applies steel or PET strap so bundles leave the line ready to load. |
Inside the mill: forming and sizing
The forming section bends flat strip into a round profile over a sequence of passes; the flower pattern is what decides how many passes and how much each one bends. The fin passes immediately before the welder do the fine work: they set the edge angle and the weld gap, which is where most seam defects are actually created.
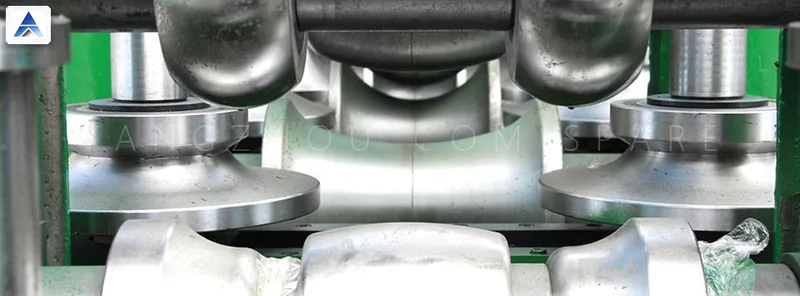
After the weld, the sizing section brings the tube to its final diameter and roundness. Sizing is not a straightener — if the tube arrives at the sizing stands oval or with a wave along the seam, the sizing stands will reproduce that error at a slightly smaller diameter. This is why we look at the whole pass line, not just the last three stands, when a mill cannot hold tolerance.
Which stations do you need?
Not every project needs nine stations, and we will not sell you the ones you do not need. Some customers start with a mill and a saw and add the packing end later; others only need a cut-off to replace a hot-saw station that is costing them scrap. Send us the pipe size range, wall thickness, material and the output you are aiming for, and we will come back with a configuration and a price for each part, so you can see exactly where the money goes.
Erection, commissioning and the handover
- Foundation and anchor plan issued before shipment, so civil work runs in parallel with production.
- Packing list checked against the crate manifest on arrival, before anything is lifted.
- Levelling and pass line alignment with a laser, recorded, not eyeballed.
- Dry run of every station, then the first welded coil at reduced speed.
- Speed ramp with a measured sample at each step: OD, wall, ovality, cut length, burr.
- Operator training on the machine they will actually run, using the setup sheets that stay in the plant.
- Handover with the signed test report, the spare parts list and the maintenance schedule.
A line is not delivered when the container clears customs. It is delivered when your operators can hold tolerance without the commissioning engineer standing next to them. We plan for that to take days, not hours, and we say so in the quotation.
Options that pay back, and options that do not
- Pay back: accumulator sized to your coil change time, quick-change stands, a spare roll set for the top-selling size, coolant temperature control.
- Pay back on export work: automatic stacker and strapping, end capping, bundle weighing.
- Usually do not: a top speed you will never run, an oversized welder for a single thin-wall product, automation on a line that runs three short orders a day.
Tell us the constraint you already know about — the saw that cannot keep up, the coil changes that eat the shift, the reject rate on one size — and the quotation will address it instead of listing everything equally.
From the knowledge centre
- What each of the nine stations decides
- Specifying a tube mill line: ten numbers for the first meeting
- Accumulator sizing: what a coil change really costs
Related products: tube mill rolls · flying cold saw · spare parts · autopacking machine.

