
HF Weld Power and Coolant: Setting Up for Thin Wall
Thin wall is where a tube mill stops being a forming machine and starts being a heat balance. Below about 1.2 mm the strip […]
Line selection, station configuration, commissioning and stability – from coil entry to the last cut.
Thin wall is where a tube mill stops being a forming machine and starts being a heat balance. Below about 1.2 mm the strip […]
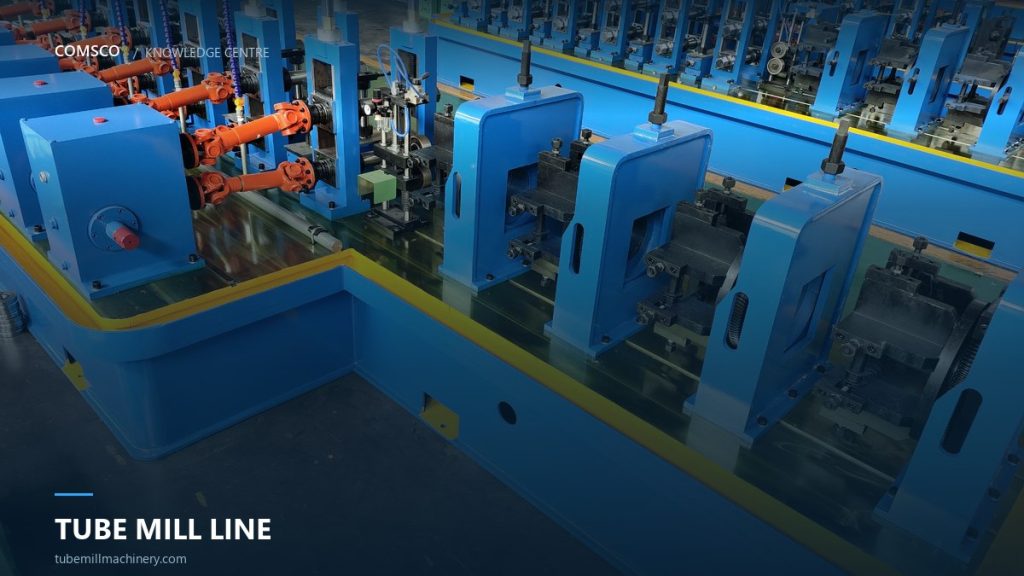
OD is correct at start-up, then creeps out of tolerance as the mill warms up. Nine times out of ten it is thermal growth, roll wear or strip width — and the order you check them in saves a shift.
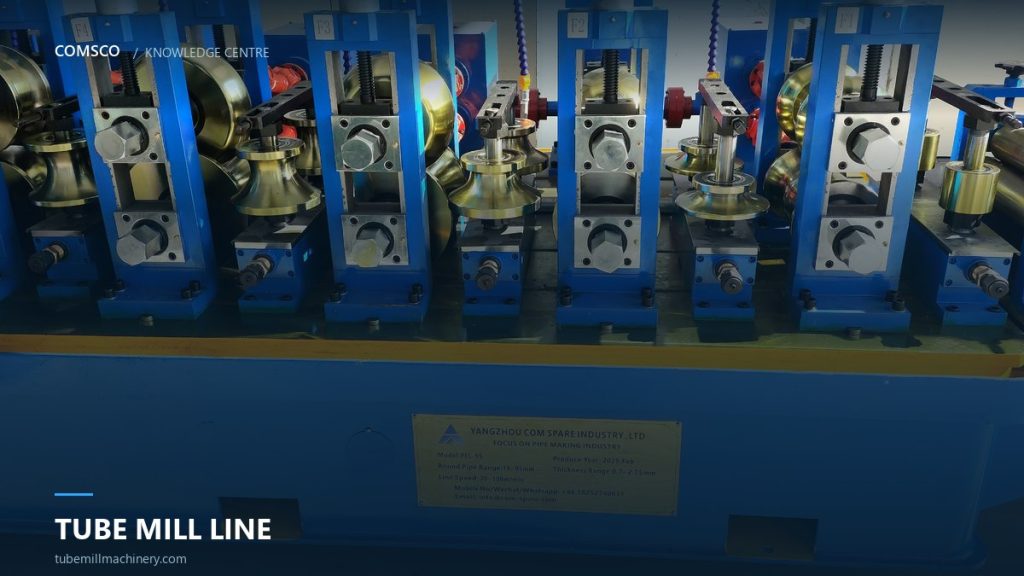
Most first quotations are wrong because the buyer sends a diameter range and nothing else. These ten numbers let a supplier size the entry section, the welder and the saw correctly the first time.
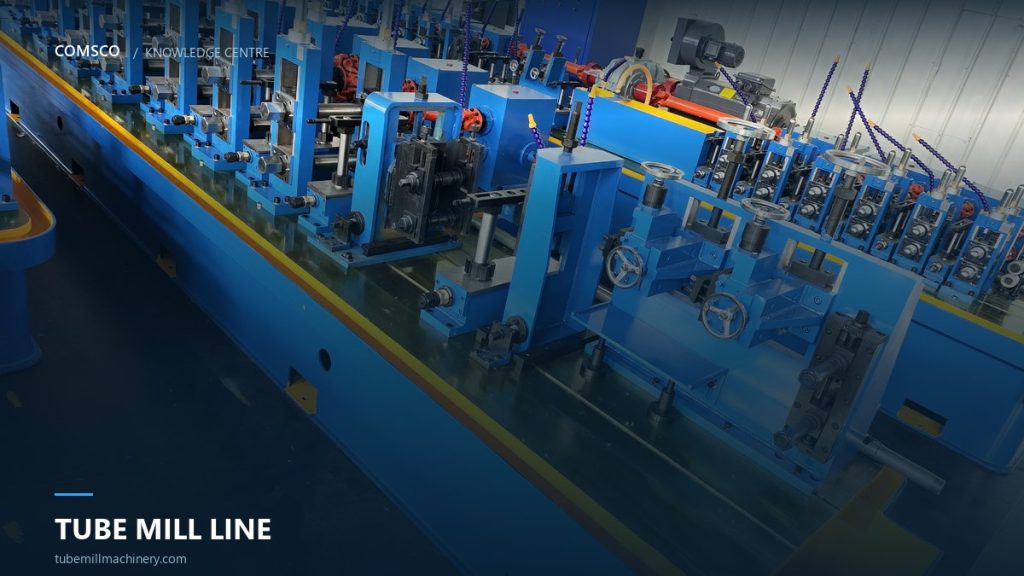
A station-by-station walk through an ERW tube mill line — what each unit controls, which tolerances it owns, and where a problem that shows up at the cut-off actually started.

