
Strip Edge Quality Before the Mill: Slitting, Burr and Weld Defects
Half the weld defects blamed on the welder are decided before the strip reaches the first stand. Edge burr, camber and width tolerance are the quiet causes.

Half the weld defects blamed on the welder are decided before the strip reaches the first stand. Edge burr, camber and width tolerance are the quiet causes.
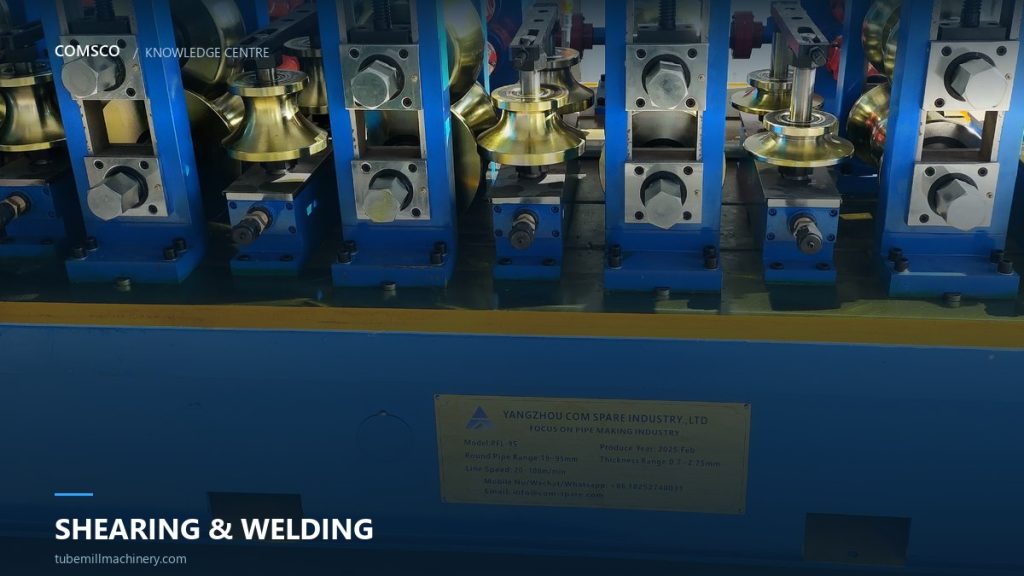
An undersized accumulator turns every coil change into a mill stop. Here is the calculation, the three accumulator types, and the mistake that makes a big accumulator behave like a small one.
The joint made at the entry section passes through every forming stand and arrives at the weld point. If defects repeat at a fixed interval, this is the machine to inspect first.
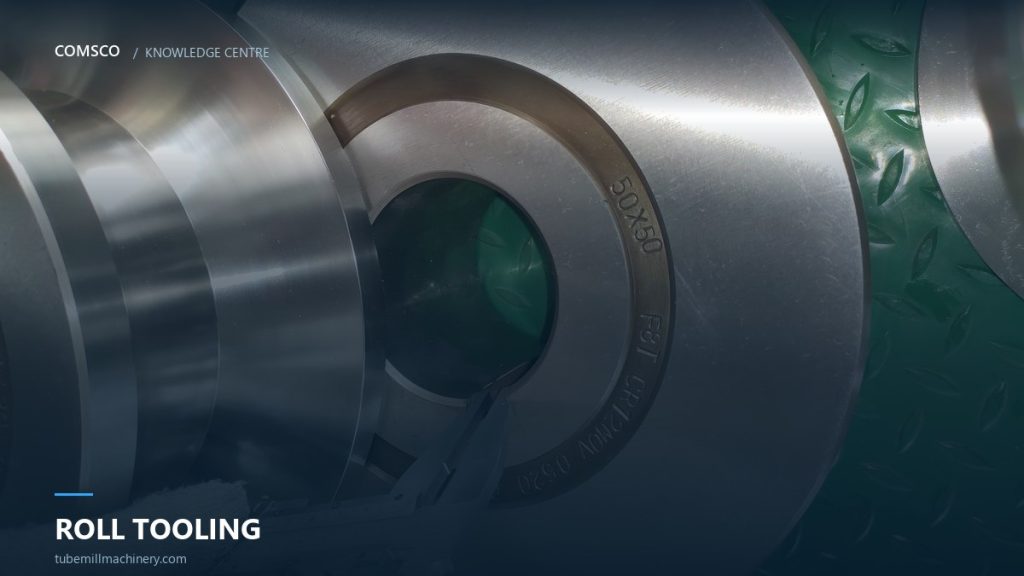
Every roll set reaches a point where the decision is no longer technical but economic. Four measurements tell you whether to regrind, adjust the pass, or order a new set.
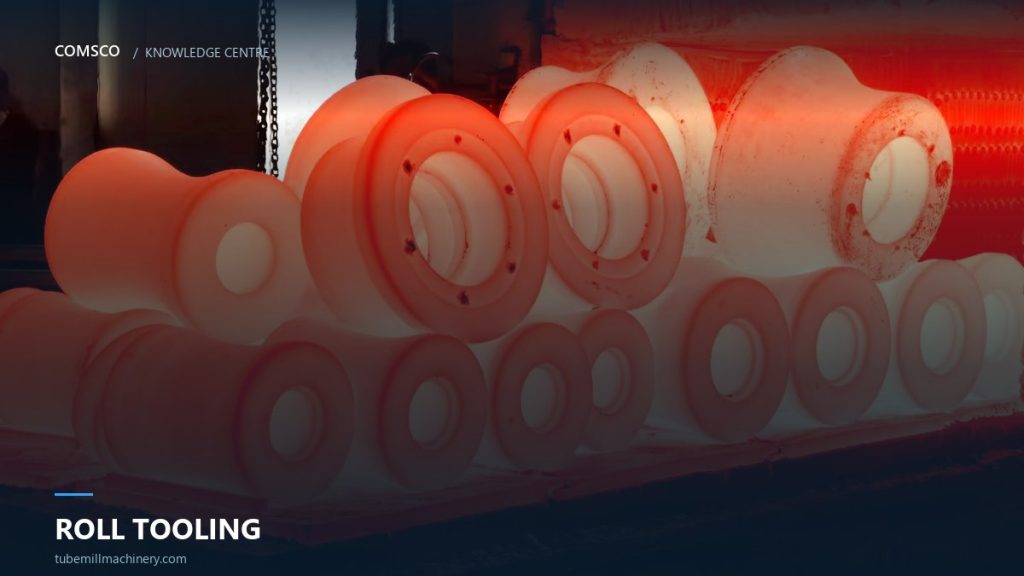
Two roll sets can look identical and last very differently. The difference is in the steel grade, the heat treatment curve and how uniformly the hardness is measured — not in the catalogue hardness.
Roll design is not a drawing exercise. It is a sequence of decisions about strip width, bend distribution and edge presentation — and mistakes only appear once the mill is running.
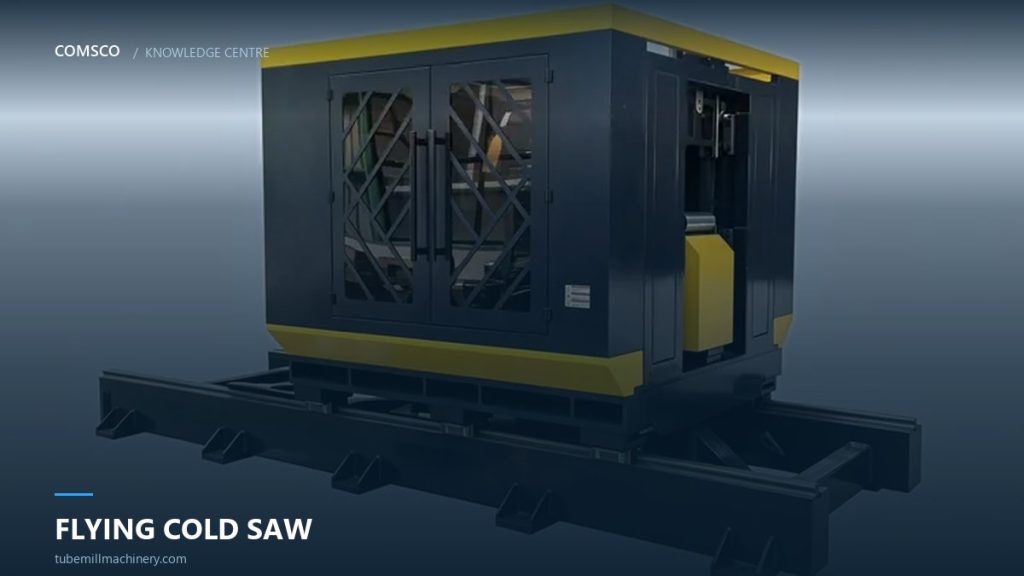
Lengths that wander by a few millimetres are rarely a blade problem. Three subsystems decide cut length — measurement, clamping and tracking — and each fails in a recognisable way.
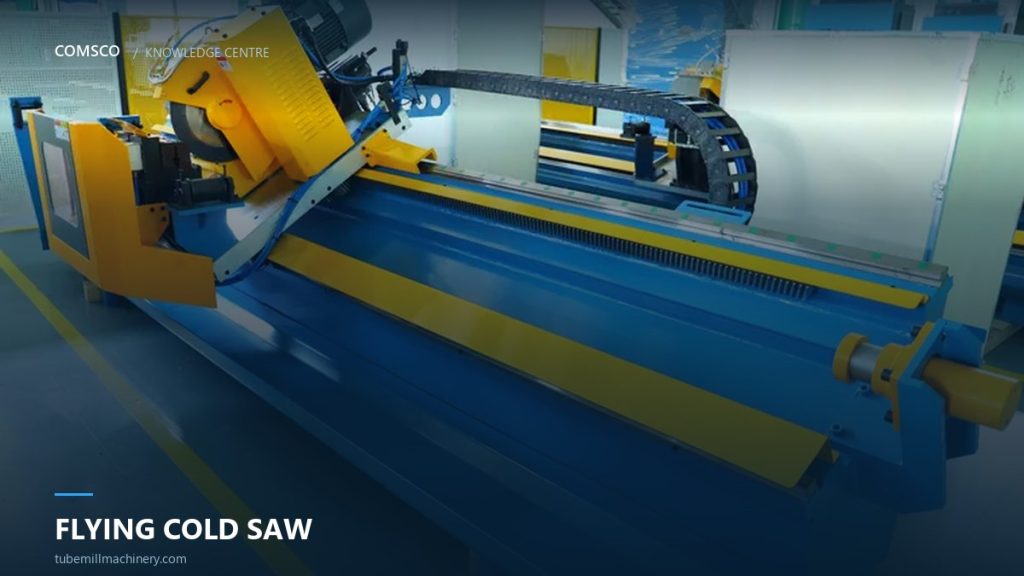
If blade consumption is eating your margin, the answer is rarely a different blade brand. Seven variables decide how many cuts a blade gives — and six of them are set on your machine.
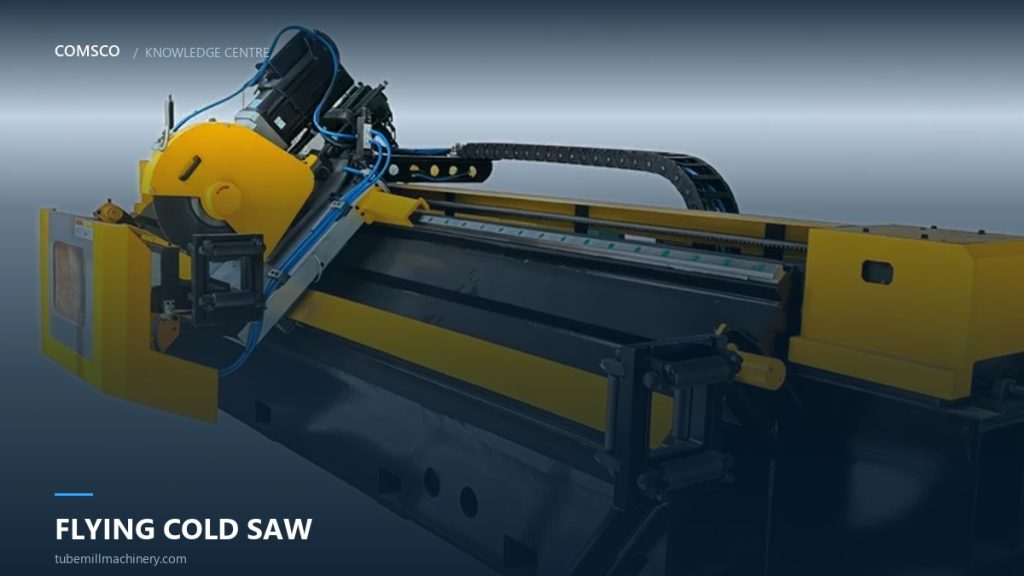
The cheap cut-off is rarely the cheap decision. A comparison of cold saw and friction saw on cut quality, secondary operations, blade cost, noise and what each one does to the tube end.
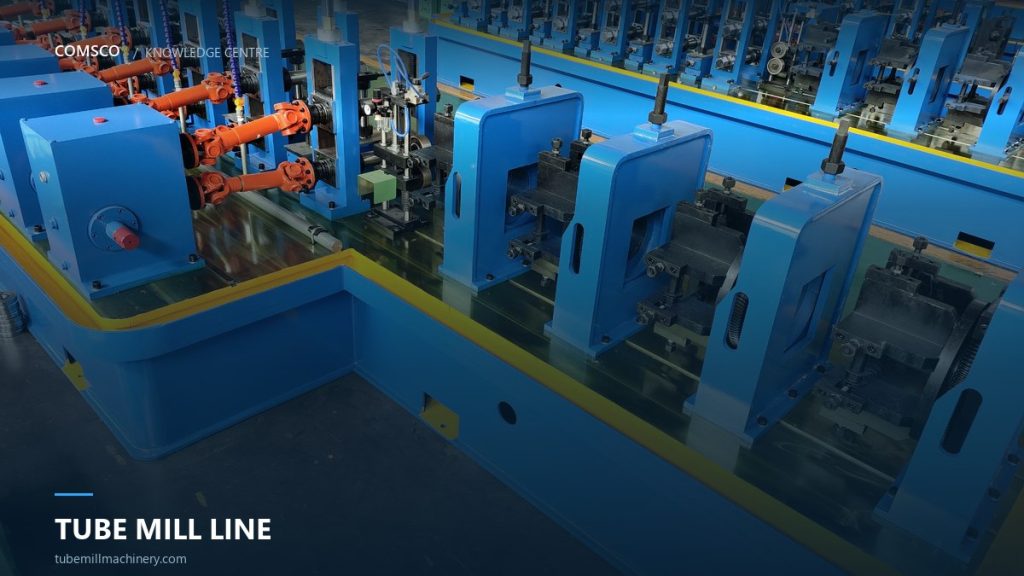
OD is correct at start-up, then creeps out of tolerance as the mill warms up. Nine times out of ten it is thermal growth, roll wear or strip width — and the order you check them in saves a shift.

