
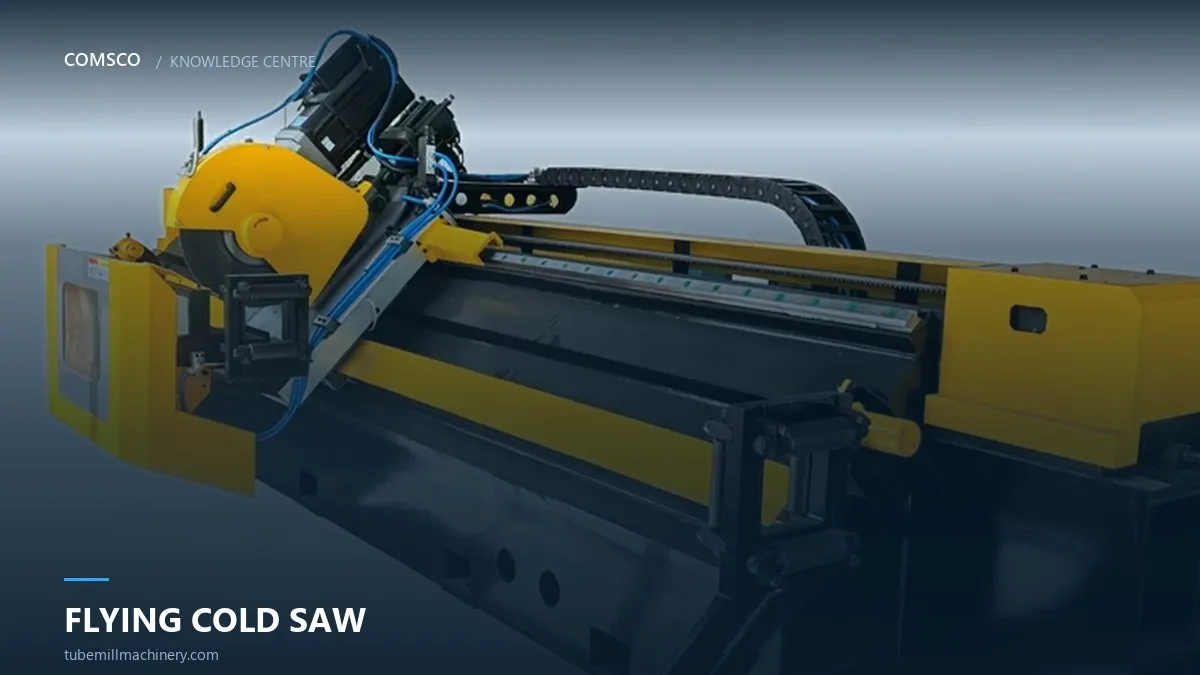
On a tube mill, the cut-off is the last operation before the tube is bundled and sold. It is also the place where the cheapest equipment decision is made — often with consequences that run for years.
The choice is usually between a flying cold saw, which mills through the wall with a toothed blade, and a friction saw, which burns through the wall with a high-speed disc. Both are called “saws”. They are not the same process, and they do not produce the same product.
Two different physics
A friction saw spins a hardened disc at very high peripheral speed. Contact friction heats the steel above its melting range and the disc throws the softened metal out of the kerf. The cut is fast and the machine is mechanically simple.
A flying cold saw turns a HSS or carbide-tipped blade at a controlled, much lower speed with high torque. Each tooth removes a chip. Heat goes into the chip rather than into the tube, so the cut face stays cool and the metallurgy of the tube end is unchanged.
Everything that follows — burr, discolouration, noise, secondary labour — comes from that single difference.
Cut face and heat-affected zone
| Friction saw | Flying cold saw | |
|---|---|---|
| Cut mechanism | Melting / burning | Chip forming |
| Heat-affected zone | Wide, visible blue discolouration | None to negligible |
| Burr | Heavy outer and inner flash | Small, usually removable in the same pass |
| Squareness | Can be good, but end is thermally stressed | Good, geometry-driven |
| Noise | Very high | Markedly lower |
| Coated / galvanised tube | Coating burns back from the cut | Coating stays intact to the edge |
For black structural tube that will be welded into a frame, a friction cut is often acceptable and the burr is dressed as part of fabrication. For tube that is sold as a finished product — furniture, scaffolding, conduit, automotive parts, stainless — the cut face is part of the product and the customer sees it.
The cost that does not appear on the quotation
Friction saw costs are mostly visible: a cheap machine and inexpensive discs. Cold saw costs are mostly visible too: a more expensive machine and more expensive blades. The difference hides in the operations around the saw.
- Deburring labour. Every friction-cut bundle needs a second operation: a deburring machine, an end-facing station, or people with a grinder. That is floor space, handling and wages, every shift.
- Scrap at the end. A thermally stressed end that cracks during expansion or threading becomes a reject at the customer, not at your mill.
- Blade cost per cut. Friction discs are cheap but short-lived and cannot be resharpened many times. Carbide blades cost more but can be resharpened repeatedly and cut thousands of tubes.
- Energy. Friction saws use large motors to generate heat. A cold saw uses a smaller high-torque drive and removes metal instead of melting it.
- Environment. Sparks, fume, fine dust and high noise are increasingly regulated. A cold saw makes chips, not smoke.
When a friction saw still makes sense
There are cases where the friction cut is the right engineering answer: very thick wall where a cold saw would be slow, low-value product where the end is never seen, or an existing line where the cut-off is not the bottleneck and capital is limited. Being honest about this is more useful than claiming one technology wins everywhere.
The rule we use: if the tube end is sold to a customer, or if any downstream operation touches it, the cold saw pays for itself. If the tube goes straight into a fabrication jig where the end is buried in a weld, the calculation is different.
What to check before choosing
- Tube size and wall range. Blade diameter and tooth count follow from the largest and smallest section you cut.
- Line speed. The saw must complete cut, retract and return within the time the line produces one length. A slow carriage becomes the bottleneck of a fast mill.
- Cut length tolerance. Servo tracking plus a robust clamp holds ±1 mm; lighter designs hold ±3 mm at best.
- Material. Carbon steel, galvanised, stainless and high-strength tube need different blade geometries and cutting parameters.
- Blade availability. A machine that only accepts an unusual blade size is a supply-chain risk.
The question to ask your supplier
Do not ask “what is the cut quality”. Ask: what burr height do you guarantee, on which wall thickness, at which line speed, and with which blade? A supplier who can answer that with numbers has tested the machine. A supplier who answers “burr-free” without a number has not.
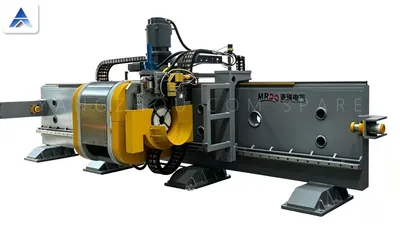
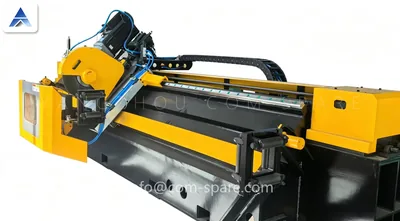
Our flying cold saw range covers ø8–377 mm tube with servo tracking and a burr-controlled cut, and the milling-type orbital cut-off page covers the large-diameter case where a conventional flying saw runs out of stroke.
Frequently asked questions
Is a flying cold saw really burr-free?
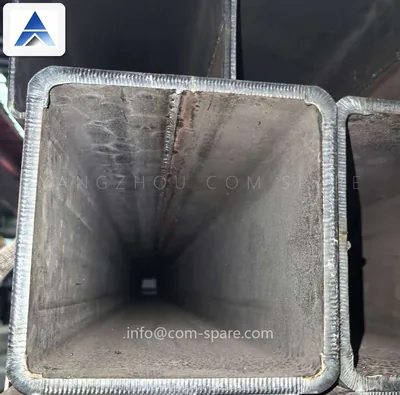
No saw is completely burr-free. A well-set cold saw keeps burr small enough that most products need no secondary operation, typically a light, uniform edge rather than the heavy flash left by a friction saw. Ask for a burr height figure at your wall thickness.
Can a cold saw cut stainless tube?
Yes, with carbide-tipped blades, lower cutting speed, negative rake geometry and adequate coolant. Stainless work-hardens, so feed and speed have to be controlled rather than forced.
Does a flying cold saw stop the production line?
No. The saw carriage accelerates to match tube speed, clamps, cuts and returns while the mill keeps running. That is the difference between a flying saw and a stationary cut-off.
Keep reading
ERW Weld Seam Defects: A Diagnostic Order That Saves Time
A tube mill with a weld problem usually gets adjusted in the order the symptoms appear, and the symptoms appear…
HF Weld Power and Coolant: Setting Up for Thin Wall
Thin wall is where a tube mill stops being a forming machine and starts being a heat balance. Below about…
Tube Mill Roll Changeover: Where the Hours Actually Go
Ask a mill manager how long a size change takes and the answer is usually a number with a shrug:…
Strip Edge Quality Before the Mill: Slitting, Burr and Weld Defects
Half the weld defects blamed on the welder are decided before the strip reaches the first stand. Edge burr, camber…
Accumulator Sizing: How Many Seconds of Strip Your Line Really Needs
An undersized accumulator turns every coil change into a mill stop. Here is the calculation, the three accumulator types, and…
Shear & End Welder: The Coil Joint That Decides Your Weld Seam
The joint made at the entry section passes through every forming stand and arrives at the weld point. If defects…
Related Products
Machines that do the job described above — quoted station by station.
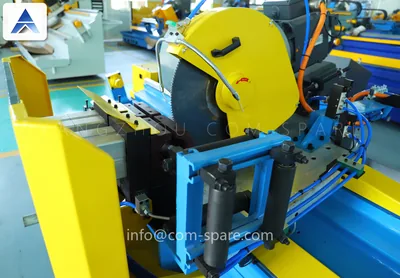 ProductFlying Cold SawBurr-free cut ends at line speed, no heat-affected zone.View specifications →
 ProductTube Mill Flying Cold SawCarriage, clamp and encoder in one frame.View specifications →
 ProductHigh Speed Flying Cut-OffShort cycle times for thin-wall, high-volume tube.View specifications →
 ProductMilling Type Orbital Cut OffOrbital milling for large OD and heavy wall.View specifications →
 ProductLaser Flying SawNo blade, no burr, no blade consumable.View specifications →
Need this checked on your own mill?
Send tube OD, wall thickness and the symptom. We reply within one working day.

