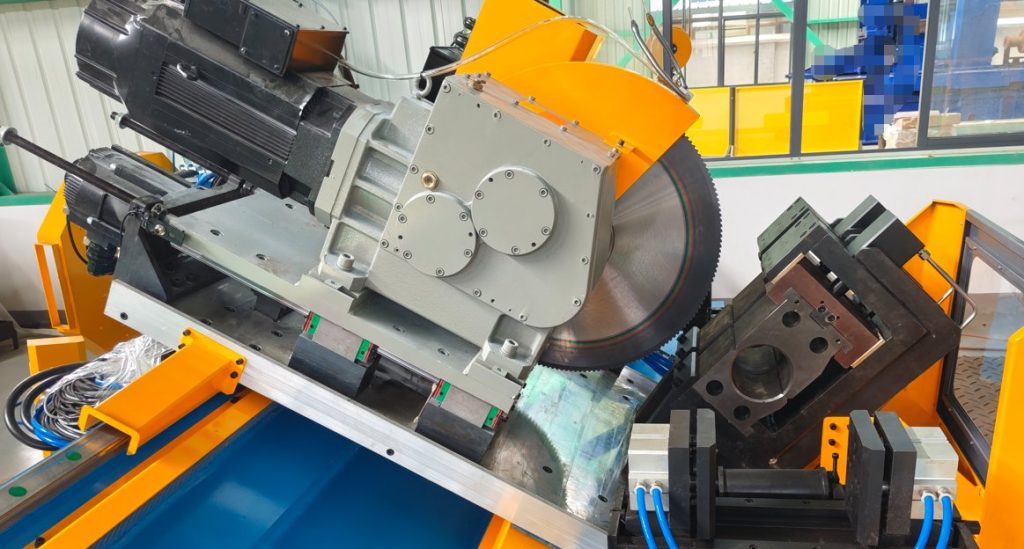
Part of our circular saw blade guide.
“TCT or HSS?” is the first question we ask when a tube mill sends a blade enquiry, and it is usually the question the buyer wants answered first as well. The two blades look similar on a shelf and behave very differently in the cut. This note gives you the decision we use in practice — by material, wall thickness and production volume — so you can shortlist a blade before you send a drawing.
If you already know what you need, our HSS & TCT circular saw blade page lists the two families, the BW/BR tooth forms and the three details we need to confirm a blade.
The short answer
Use HSS for mild carbon steel in thin to medium walls, especially where you want low cost per cut and re-grind the blade in-house. Use TCT for large diameters, heavy wall, stainless or high-strength steel, and for long production runs where blade changes cost more than the blade itself. Wall thickness and material grade decide the family; the flying saw cycle decides the tooth form.
What each blade actually is
HSS (High-Speed Steel) blades are cut from a single piece of high-speed tool steel. The whole tooth is the same material, so the blade can be re-ground several times on a blade grinder and returned to service. That is why HSS stays economical in long runs on friendly material.
TCT (Tungsten Carbide Tipped) blades have carbide tips brazed onto a steel body. The carbide edge holds its hardness far longer than tool steel under heat and abrasion. TCT is the answer when the material or the wall punishes an HSS edge. It is normally replaced or professionally re-tipped rather than ground in your own workshop.
Choose by material and wall thickness
This is the single most reliable way to choose. Material and wall together decide the grade; the cycle time then decides the tooth count and pitch.
| Material / job | Wall | Recommended family | Why |
|---|---|---|---|
| Mild carbon steel, general tube | Thin to medium | HSS | Clean end face, low cost per cut, re-grindable |
| Mild carbon steel, heavy section | Thick | TCT or HSS | Chip clearance and edge life matter more |
| Stainless / alloy steel | Any | TCT | Carbide resists abrasion and work hardening |
| High-strength steel | Medium to thick | TCT | HSS edge softens at the speeds required |
| Fully automatic flying saw | Any | HSS or TCT, BR form | Chip breaker protects the cut face in automatic cycles |
Choose by diameter and production volume
Diameter and volume are the second filter. As blade diameter grows, the edge speed at the rim rises for the same spindle speed, and an HSS edge gives up hardness faster. Above roughly the medium diameter range, TCT becomes the safer choice even on mild steel if the line runs continuously.
Volume changes the economics. On a short job or a tube size you run occasionally, a cheaper HSS blade that you can re-grind is often the rational buy. On a line that cuts around the clock, an unplanned blade change stops the whole mill, and the longer life of TCT pays for itself even though the blade costs more up front.
Do not forget the tooth form
Grade is only half the decision. The tooth form decides how the chip is broken and cleared. For tube cutting saws two forms cover most production: BW, the standard alternating bevel for general pipe cutting, and BR, the chip-breaker form preferred on fully automatic flying saws. A correct grade with the wrong form still gives a poor cut face. Both forms are illustrated on our blade page.
Cost per cut, not price per blade
The tempting comparison is the purchase price, but a blade that costs half as much and lasts a quarter as long is the expensive option once you add changeover time and scrap. Judge a blade by cost per cut: purchase price plus re-grinding divided by the cuts it delivers at an acceptable end face. This is also why speed, feed and clamping — not the supplier logo — so often decide whether a blade “wears out early”.
Three details to send for a recommendation
- Tube material and grade — carbon, alloy or high-strength, and the grade if you have it.
- Tube outside diameter and wall thickness — these decide diameter, tooth count and pitch.
- Current blade size — OD × ID × thickness × pin hole, or a drawing / sample.
With those three details we will confirm HSS or TCT, the tooth form, and what we can supply against your current blade. Our flying cold saws and the blades for them are built and matched in our own workshop. Send your details here.
Frequently asked questions
Is TCT always better than HSS?
No. On thin to medium wall carbon steel, HSS gives a clean cut at lower cost per cut and can be re-ground. TCT wins on hard material, heavy wall, large diameter and long runs — not on every job.
Can HSS blades cut stainless steel?
They can, but edge life is short. For stainless and alloy grades a TCT blade is the usual recommendation because the carbide edge resists abrasion and work hardening.
How many times can an HSS blade be re-ground?
Several times, depending on the remaining tooth body and how much material is removed each grind. Re-grinding on a proper blade grinder is what keeps HSS economical.
What is the difference between BW and BR tooth forms?
BW is the standard alternating bevel for general pipe cutting and moderate walls. BR adds a chip-breaker groove for cleaner chips and a better cut face, and is preferred on fully automatic flying saws.
Do you supply blades for saws that are not yours?
Yes. Send your saw model and the blade drawing or a sample, and we will confirm the size, bore and tooth form we can supply.
Related reading
Saw Blade Life on a Flying Cold Saw: Seven Variables You Can Control · Flying Cold Saw vs Friction Saw · HSS & TCT Circular Saw Blades
Keep reading
Cut Length Tolerance on a Flying Cold Saw: Encoder, Clamp and Carriage
Lengths that wander by a few millimetres are rarely a blade problem. Three subsystems decide cut length — measurement, clamping…
Saw Blade Life on a Flying Cold Saw: Seven Variables You Can Control
If blade consumption is eating your margin, the answer is rarely a different blade brand. Seven variables decide how many…
Flying Cold Saw vs Friction Saw: What the Cut Face Really Costs
The cheap cut-off is rarely the cheap decision. A comparison of cold saw and friction saw on cut quality, secondary…
Related Products
Machines that do the job described above — quoted station by station.
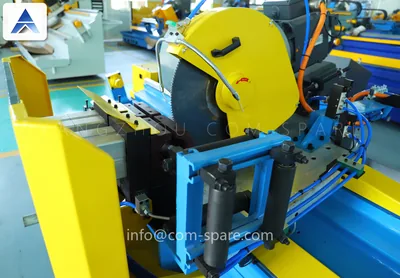 ProductFlying Cold SawBurr-free cut ends at line speed, no heat-affected zone.View specifications →
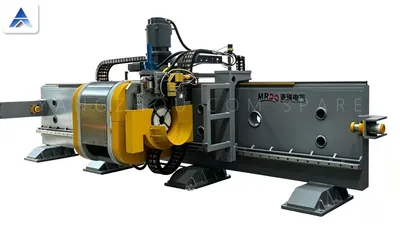 ProductFlying Cold Saw — Ø16 – Ø273 mm, Rack Drive, -P / -H ClampCarriage, clamp and encoder in one frame.View specifications →
 ProductHigh-Speed Flying Cold Saw — Ø16 – Ø140 mm, Timing Belt DriveShort cycle times for thin-wall, high-volume tube.View specifications →
 ProductMilling Type Flying Cut-Off — Ø89 – Ø508 mm, Twin BladeOrbital milling for large OD and heavy wall.View specifications →
 ProductLaser Flying Saw — Ø16 – Ø630 mm, No Blade, No BurrNo blade, no burr, no blade consumable.View specifications →
Need this checked on your own mill?
Send tube OD, wall thickness and the symptom. We reply within one working day.